TERRY TOWEL
ABC for Terry Towel
Planning for integrated terry towel mills, from yarn dyeing to cutting, sewing and packing.
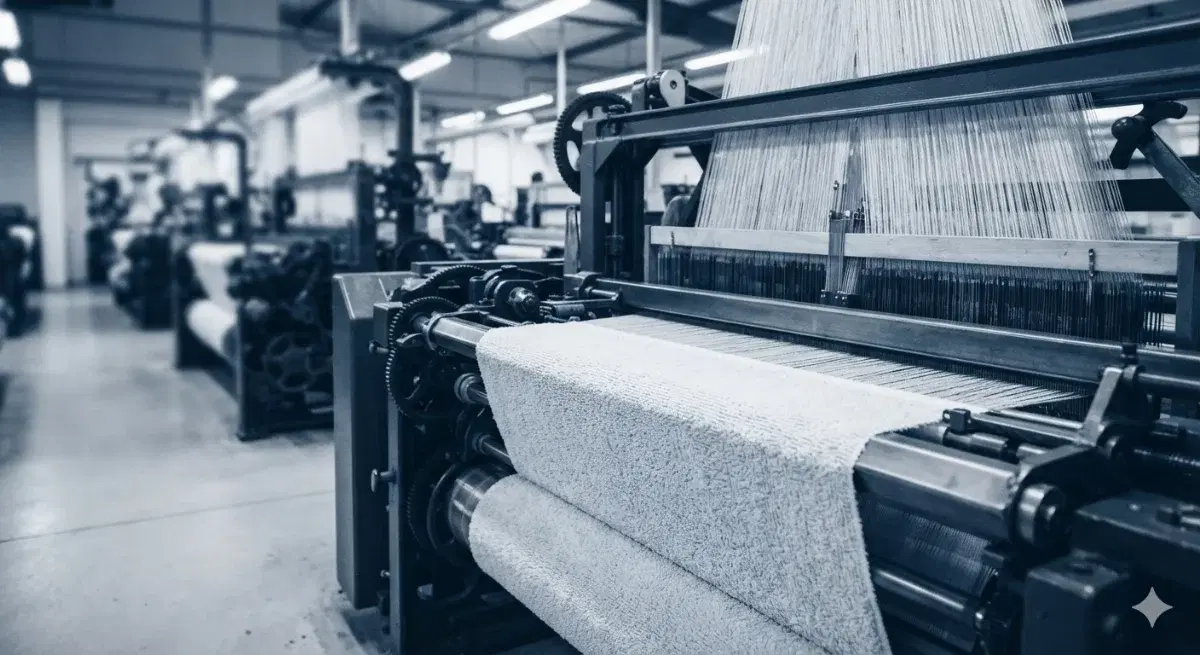
THE PROBLEMS WE SOLVE
Where planning loses money in terry towel today.
palette
Dye Lots That Don't Match Demand
Yarn is dyed in lot sizes that leave shade remnants or short orders.
grid_on
Changeovers Decided Loom by Loom
Quality and size changes are sequenced by hand across many looms, so changeover time is never minimised.
invert_colors
Batches Filled by Rule of Thumb
Dyeing batches are filled to capacity, not to due date or shade sequence.
timeline
One Delay Moves Everything
A late yarn lot pushes looms, dyeing and dispatch, and nobody sees it until dispatch.
precision_manufacturing
APS
Planning follows the mill's route: Yarn Dyeing, Warping, Weaving (Loom Planner), Processing, then Cutting, Sewing & Packing.
LIVE MODULES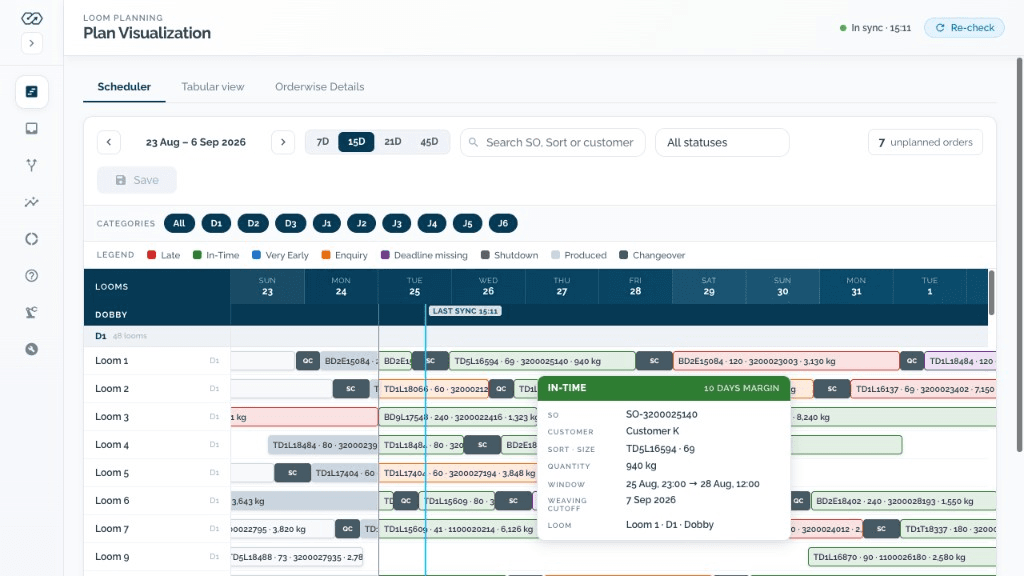
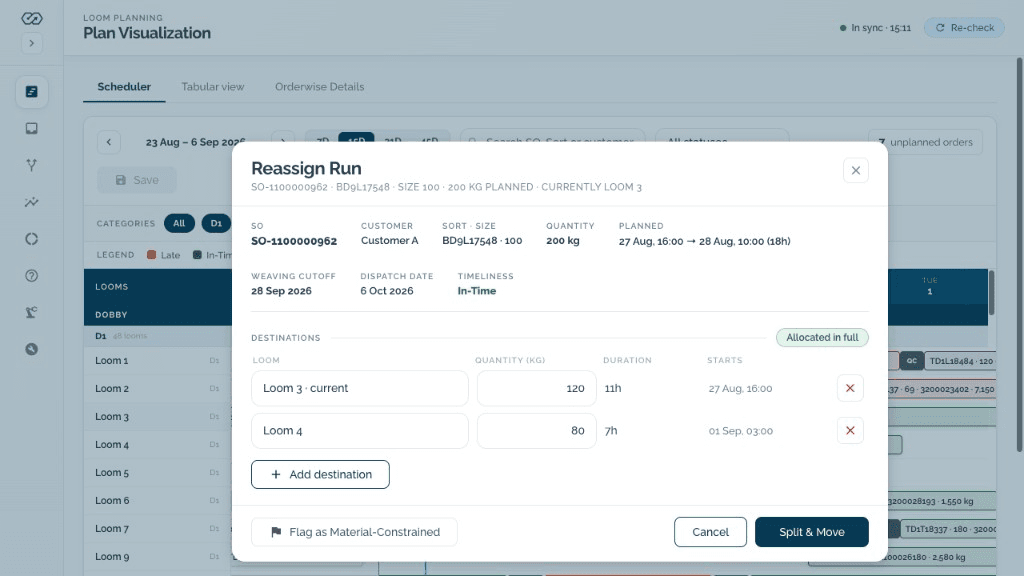
- 01One live plan across every loom
- 02Cutoffs first, then the least changeover time
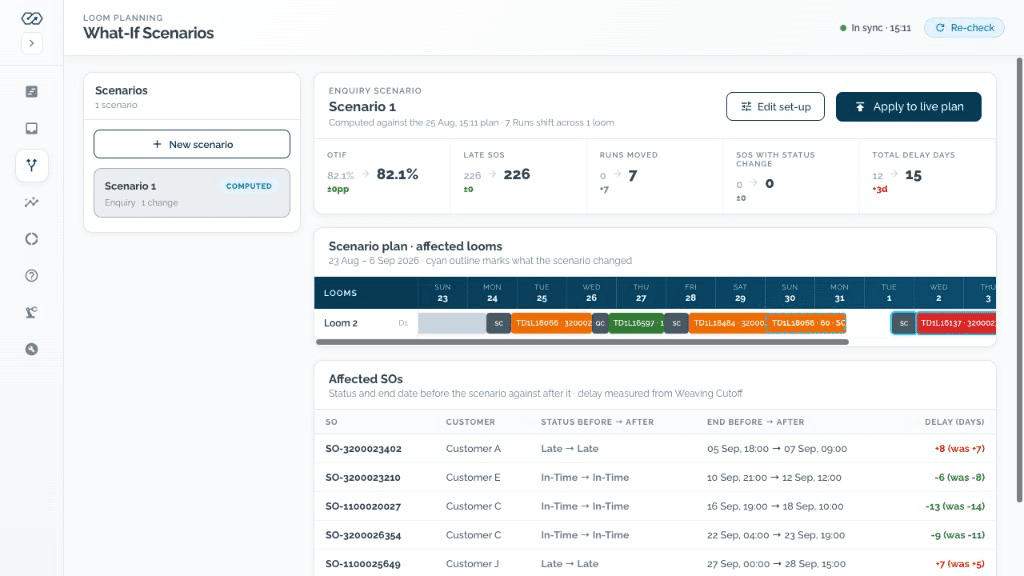
- 03What-if scenarios beside the live plan
- 04Loom eligibility enforced, exceptions logged
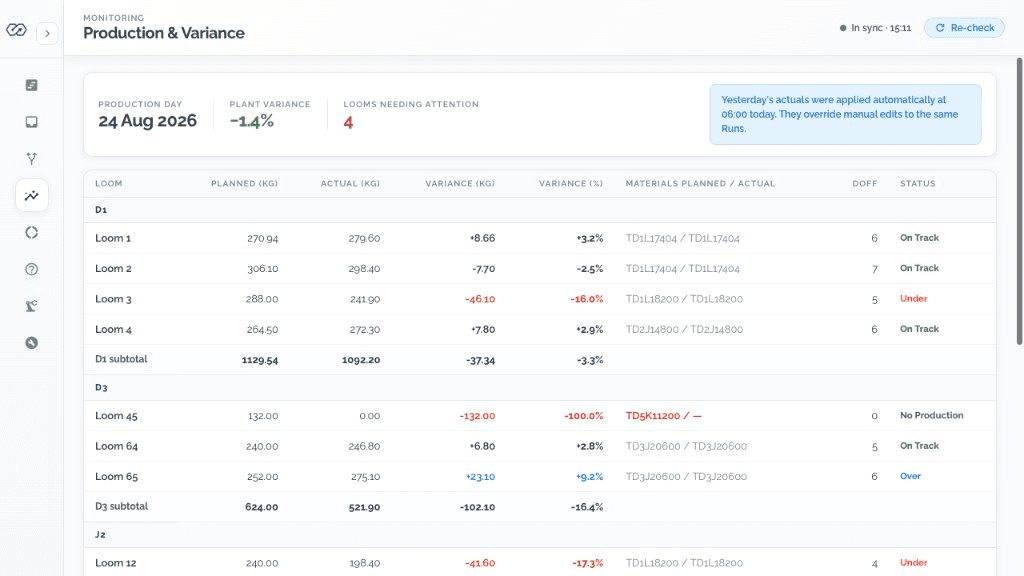
- 05Planned versus actual production by loom
COMING SOON
palette
Yarn Dyeing PlannerPlans yarn dye lots against weaving demand.
timeline
Warping PlannerPlans warp beam preparation ahead of weaving.
invert_colors
Processing PlannerPlans post-weaving processing of woven fabric.
content_cut
CSP PlannerPlans cutting, sewing and packing through to dispatch.